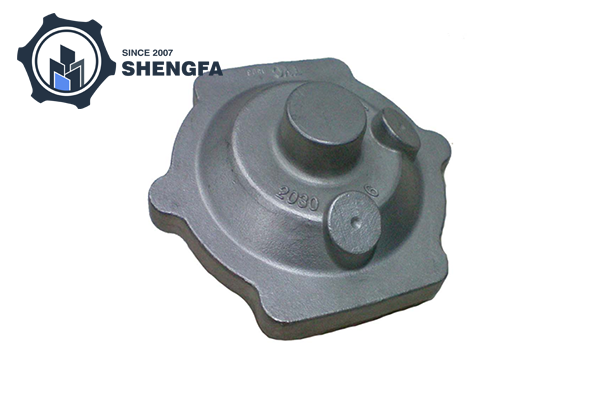
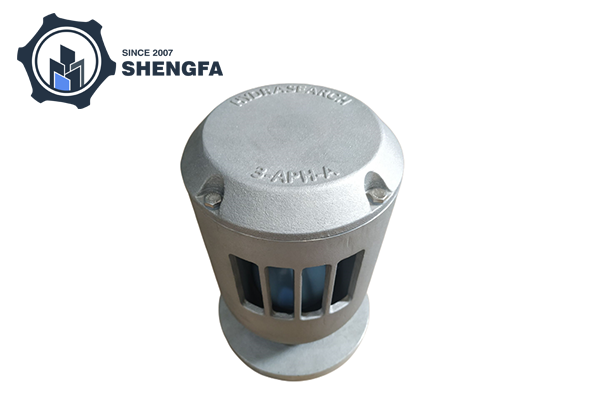
SHENGFA Low Alloy Steel Investment Castings are designed for industrial components requiring cast-steel strength, complex geometry, and CNC-machined mounting features.
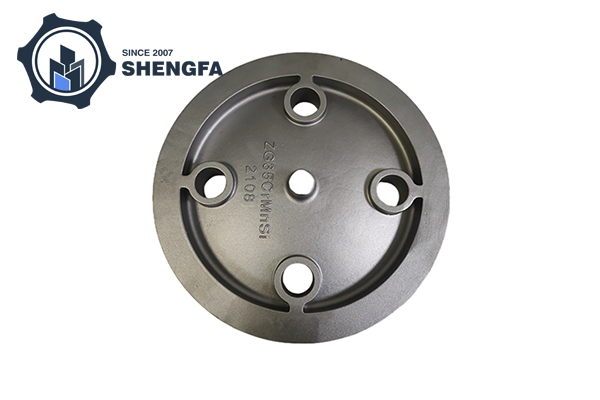
SHENGFA low alloy steel investment castings combine alloy steel construction with near-net-shape forming and secondary machining.
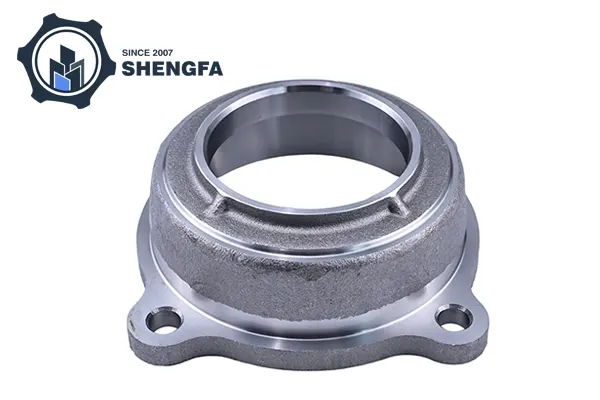
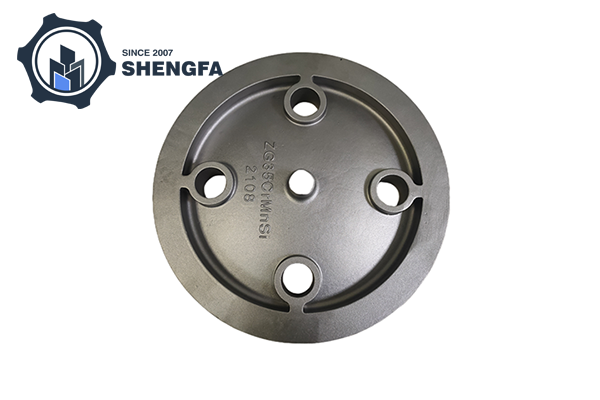
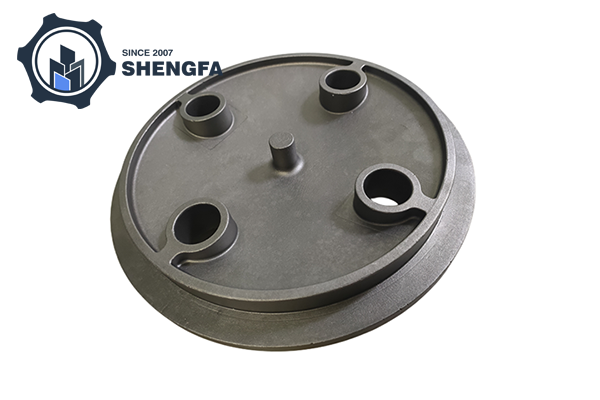
The reference component is a circular flange or connecting disc marked ZG35CrMnSi. Its structure includes one central locating hole, four circumferential bolt holes with clearance recesses, and an internal annular groove. The supplied part has an unpainted, matte metallic as-cast surface and can be CNC machined for finished dimensions and mating interfaces.
The reference casting uses ZG35CrMnSi, a chromium-manganese-silicon alloy cast steel designation. The material is associated with engineering components requiring strength, toughness, and resistance to impact and wear.
| Material designation | Selection considerations |
|---|---|
| ZG35CrMnSi | Reference casting grade for mechanical components exposed to loads and impact. Final properties depend on composition, casting quality, and heat treatment. |
| Carbon steel | Suitable for applications where the specified carbon content and mechanical properties meet the component requirements. |
| Low alloy steel | Selected for required strength, toughness, hardenability, and wear performance according to the specific grade. |
| Stainless steel alloy | Considered where corrosion resistance is a primary material requirement. |
In the marking ZG35CrMnSi, ZG identifies cast steel, while 35CrMnSi identifies the alloy designation. The supplied reference associates this grade with JB/ZQ 4297. The additional marking 2108 is identified as a mold number, drawing number, or batch identifier rather than a material grade.
Material selection should follow the specified standard and required mechanical properties. SHENGFA's listed material-standard coverage includes GB, ASTM, AISI, DIN, BS, JIS, NF, and AAR. Grade equivalence should be established from applicable material requirements rather than assumed from similar naming.
The following table summarizes SHENGFA's supplied general manufacturing capabilities.
| Parameter | Specification |
|---|---|
| Casting process | Lost-wax investment casting |
| Casting tolerance | CT7 |
| As-cast surface roughness | Ra 12.5 μm |
| Casting weight range | 0.1–90 kg |
| Maximum linear casting size | 1,200 mm |
| Maximum casting diameter | 600 mm |
| Machining positioning accuracy | 0.008 mm |
| Repeat positioning accuracy | 0.006 mm |
| Machined surface roughness | Ra 0.8–6.3 μm |
| Maximum spindle travel | 1,800 × 850 × 700 mm |
| Maximum turning diameter | 1,000 mm |
| Available finishing | KTL (e-coating), zinc plating, mirror polishing, sand blasting, acid pickling, black oxide, painting, hot galvanizing, powder coating, nickel plating |
| Additional processing | Heat treatment, assembly, hot isostatic processing |
| Service | OEM and ODM |
For flange-style components, the machining plan can cover the central locating hole, four-hole mounting pattern, annular groove, and mating surfaces. Critical dimensions, hole positions, flatness, concentricity, and surface finish should be specified on the component drawing.
CT7 is the supplied casting tolerance designation. The listed machine positioning figures describe equipment capability; they do not establish the dimensional tolerance of every finished part. Final acceptance requirements should be defined for the individual component.
SHENGFA's stated application range covers the following industrial components:
The reference flange-style casting is suited for evaluation in mechanical connection and mounting applications where its dimensions, material condition, and load requirements match the equipment design. Pressure-containing and safety-critical applications require the applicable material, testing, and acceptance specifications.
| Comparison factor | Investment casting | Forging | Billet machining |
|---|---|---|---|
| Component geometry | Complex contours, grooves, and integrated features | Shapes suited to the selected forging process | Geometry formed by material removal |
| Material removal | Can reduce machining stock through near-net-shape forming | Machining may be needed for final interfaces | Material removed from solid stock |
| Tooling | Casting pattern and tooling required | Forging dies required for die forging | Fixtures, programming, and cutting tools required |
| Final dimensions | CNC machining for critical features | Machining for precision interfaces | Dimensions established through machining |
| Suitable considerations | Complex shapes and integrated cast features | Components whose mechanical requirements favor forging | Low-volume parts or geometries suited to machining |
For a flange or connecting disc with a central locating hole, multiple bolt holes, and an annular groove, investment casting can form the main geometry before CNC finishing. Forging or billet machining may be more suitable when the component's mechanical requirements, geometry, production volume, or tooling economics favor those processes.
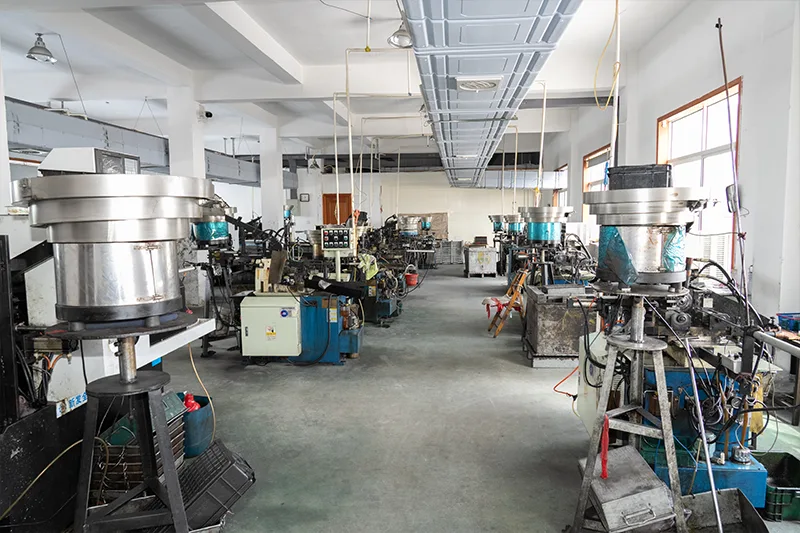
Ningbo Shengfa Hardware's stated equipment includes CNC turning machines, CNC machining centers, X-ray inspection machines, coordinate measuring machines (CMMs), 2D optical projectors, ultrasonic cleaning machines, and surface roughness testers.
These resources support inspection of internal casting features, component dimensions, profiles, and surface finish. SHENGFA states that it performs 100% inspection before packing. The inspection scope for each part can be defined around drawing dimensions, material requirements, machining features, and specified surface treatments.
Available secondary operations include CNC machining, heat treatment, plating, assembly, and hot isostatic processing. The required process sequence depends on the component design and technical specification.
To assess a low alloy steel casting project, provide the following technical information:
SHENGFA can coordinate casting and secondary machining within one production route, supporting components that require both formed geometry and finished mounting features.
SHENGFA Low Alloy Steel Investment Castings cover industrial cast-steel components requiring specified alloy grades, near-net-shape production, and CNC finishing. Submit the component drawing, material designation, order quantity, machining requirements, and inspection criteria for a project-specific quotation.
Ningbo Shengfa Hardware combines investment casting with CNC machining and secondary processing for mechanical parts, including flange-style connections, equipment housings, and heavy-machinery components. Low Alloy Steel Investment Castings can be evaluated against the component's geometry, material requirements, finished dimensions, and production volume. Please send an inquiry or contact us for further details.
Address
Yunlong Town, Ningbo City,Zhejiang Province, China
Tel